- Company
- Products
- Technical report
- Indusrial cleaning
- Micro Joining and Assembly Technology
- Ultrasonic technology
- Trouble solution
- Cleaning
- Removing
- Attaching
- PCB Columns
Published on :
In the reflow process used for electronics assembly, solder is supplied to PCB pads, electronic components are placed on the deposits, and the assembly is heated in a reflow oven to form solder joints. Solder can be supplied in several ways, including solder paste dispensing through a metal stencil or dispenser, precoated solder, and solder balls. Among these methods, stencil printing of solder paste is widely used in surface-mount assembly.
This page explains metal stencils, the solder paste printing process, common printing defects, and stencil cleaning.
Printing masks used in manufacturing can be broadly divided into the following types.
| Mesh Screen Mask (Screen Mask) |
A woven synthetic- or metal-fiber mesh with patterned openings formed using an emulsion. |
|---|---|
| Metal Stencil (Stencil) |
A thin metal sheet with patterned apertures, mounted in a frame. |
Metal stencils are commonly used for solder paste printing in electronics assembly because they support accurate, repeatable paste deposition.
 |
In surface-mount assembly, solder paste is commonly deposited using a stencil printer such as the equipment shown here. |
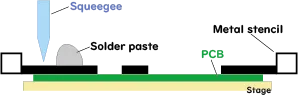 |
The PCB is positioned beneath the metal stencil and aligned with the stencil apertures. |
 |
|
 |
The squeegee moves across the stencil under controlled pressure, filling the apertures and depositing solder paste at the specified PCB locations. |
|
|
 |
The PCB and stencil are separated after printing. Solder paste deposits corresponding to the stencil apertures remain on the PCB pads. If excessive solder paste remains inside the apertures instead of transferring to the PCB, transfer efficiency decreases and the printed paste volume can become insufficient. |
Stable solder paste deposition with the required shape and volume is essential to the SMT printing process.
The following sections introduce examples of printing problems associated with stencil release and paste transfer.
For repeatable printing, stencil apertures should release solder paste consistently. Aperture geometry, wall quality, stencil condition, solder paste properties, printer setup, squeegee conditions, and board support can all affect transfer efficiency. Industry technical literature identifies aperture area ratio and transfer efficiency as important metrics in solder paste printing.
As component pitches become finer and stencil apertures become smaller, some solder paste may remain in the aperture instead of transferring to the PCB. Repeated printing under these conditions can result in deposits with insufficient or inconsistent volume. Paste remaining in an aperture may also later be released unexpectedly, producing an excessive local deposit.
If there is a gap between the stencil and PCB surface, or if printing conditions such as squeegee pressure are inappropriate, solder paste can spread beyond the intended aperture area. Excessive squeegee pressure can also disturb the stencil or printing setup and contribute to variation in transfer efficiency.
Smearing or other unintended paste deposits can contribute to soldering defects such as bridging. Maintaining suitable printing conditions and keeping the stencil clean are therefore important parts of process control.
Metal stencils should be cleaned at suitable intervals to maintain consistent aperture condition and solder paste transfer.
KAKEN TECH has compared cleaning of contaminated metal stencils using IPA, HA-4900 metal stencil cleaning spray, and ultrasonic cleaning. The results are introduced on the following page.
 |
Technical Solutions
|
|---|
What should you consider when selecting a cleaner for metal stencils?
The appropriate cleaner depends on the paste being removed, stencil construction, cleaning method, workplace requirements, and applicable regulations. Four key considerations are introduced below.
IPA is still used in some workplaces for manual stencil wiping. However, as stencil apertures become smaller, the cleaning agent must remove solder paste effectively from fine apertures.
Select a cleaner with sufficient solder paste removal performance for the paste formulation and cleaning method. Dedicated metal stencil cleaners, including glycol-ether-based formulations, are among the options used for this purpose.
A framed metal stencil can include the metal stencil foil, frame, mesh or other tensioning structure, and adhesive tapes or bonding materials.
The cleaner should remove the target paste while remaining compatible with the stencil materials and construction.
For example, if a cleaner adversely affects bonding materials or tape, stencil tension or mechanical integrity may be affected. Compatibility should therefore be checked under the actual cleaning conditions.
Worker exposure and environmental characteristics should also be considered when selecting a cleaning agent. Relevant factors can include VOC emissions, odor, skin-contact hazards, flammability, waste handling, and environmental impact. Review the latest SDS and applicable workplace requirements for the country or region where the cleaner will be used.
Cleaning-agent regulations differ by country and region and can change over time. Depending on the formulation and quantity used, requirements may apply to storage, ventilation, fire protection, worker exposure, emissions, or waste management.
IPA, for example, is a flammable solvent and requires appropriate controls based on the applicable SDS, local regulations, use conditions, quantities, and equipment configuration.
When selecting a cleaner, review its current SDS and confirm all applicable legal and workplace-safety requirements in the location of use.
 |
Product Information
|
|---|
Standard Micro-Soldering Technology, 3rd Edition
Edited by the Micro Soldering Education Committee, Japan Welding Engineering Society
The Nikkan Kogyo Shimbun, Ltd.
|
Technical Solutions
|
|---|---|
 |
Published Technical Article
|
| Please be as specific as possible in your inquiry. Depending on the contents of your inquiry, it may take some time for us to reply to you. If you need product documentation (SDS/safety data sheets, TDS, instruction manuals, etc.), please contact us via “Request for SDS and other product documentation” ※Sales message through the inquiry form are strictly prohibited. |
KAKEN TECH, MICROCLEANER, MICROCLEAN&MARKLESS and MARKLESS are trademarks of KAKEN TECH CO., LTD. in PRC.
KAKEN TECH is a trademark of KAKEN TECH CO., LTD. in the U.S..
 Inquiry form
