- Company
- Products
- Technical report
- Indusrial cleaning
- Micro Joining and Assembly Technology
- Ultrasonic technology
- Trouble solution
- Cleaning
- Removing
- Attaching
- PCB Columns
Published on :
Cratering is a coating defect that occurs when a substance with lower surface tension than the liquid paint comes into contact with the coating. The contaminant spreads as it is drawn across the paint surface, causing the coating film to become locally thinner. A similar defect can also occur when uncured paint mist falls onto a wet coating film, dissolves in the thinner contained in the coating, and displaces the surrounding paint as it spreads. Cratering can occur in many coating processes, not only automotive painting. This page introduces cratering cases, possible causes, and troubleshooting approaches for coating processes in general.
When injection-molded resin products are painted, external mold release agents sprayed during molding and condensed substances from internal mold release agents incorporated into resin pellets can become causes of cratering. When subsequent painting is planned, paintable external mold release agents are generally selected. Internal mold release agents may be compounded into the pellets together with additives such as antistatic agents so that external mold release can be reduced or eliminated. If these release-agent components are present only as very small amounts and remain sufficiently dispersed, they may not cause visible cratering. However, if they concentrate or form larger agglomerates, cratering can occur.
When external mold release agents are used during injection molding, operators may apply more release agent around complex shapes and edges than on flat areas to improve mold release. Even when internal mold release agents are normally used, a small amount of external mold release agent may be applied to areas with poor release during initial machine startup or after mold cleaning. Problems can also occur when startup parts or stored molded parts are exposed to mold-release spray mist. When investigating cratering, it is therefore useful to check not only the painting process but also the injection-molding and storage processes.
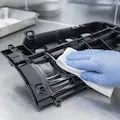
When the surfaces of injection-molded resin parts are wiped with cloths or sponges impregnated with IPA (isopropyl alcohol) or solvent-based wiping agents to remove dust and contamination, splash-like or streak-like cratering may occur on flat surfaces. Splash-like defects may correspond to the points where the operator first places the cloth on the workpiece or stops wiping. At these locations, the wiping liquid can remain locally and contamination can become concentrated as the liquid dries. Multiple streak-like defects can also appear when too much wiping agent is applied and the liquid dries along wiping marks.
As described above, internal mold release agents and antistatic additives may already be incorporated into the resin. If wiping liquid remains wet on the resin surface for an extended period, these additives may be extracted into the wiping agent and become concentrated as the liquid dries, potentially creating cratering contaminants. To reduce this risk, use an appropriate amount of wiping agent and avoid stopping the cloth on the workpiece during wiping. A suitable wiping agent should wet the surface evenly and dry uniformly. If the agent beads up, dries in splash-like patterns, or leaves water marks, the wiping agent and application conditions should be reviewed. The wiping solution should also be replaced before accumulated contamination becomes excessive.
The material, fiber shape, and weave of the wiping cloth are also important. Select the cloth after confirming compatibility with the wiping agent and the workpiece.
If clothing from molding and painting departments is washed or dried in the same equipment, mold release agents from the molding area may transfer to clothing used in the painting area.
Many materials used around a painting area can affect coating quality even when workers are unaware that they contain substances capable of causing cratering.
Silicone, a well-known cause of cratering in coating processes, can be found in a wide range of products such as shoe polish, glass cleaners, defoamers, automotive waxes, heat-resistant greases, and some other products. Understanding where silicone-containing materials are used and controlling possible transfer routes are important when troubleshooting cratering.
Cratering can occur if silicone-containing materials remain on workers or their clothing when coating operations begin.
| Examples of Possible Silicone Sources | Possible Source Activity |
|---|---|
| Silicone in automotive wax | Waxing a vehicle |
| Silicone in shoe polish | Polishing leather shoes |
| Silicone in hair-care products | Hair styling |
| Silicone-containing surface treatment on printed materials | Handling magazines or advertising inserts |
| Silicone in glass cleaners | Cleaning offices or production areas |
Some cratering problems may appear only under particular airflow or weather conditions, suggesting that airborne contamination is being carried toward the painting area.
| Examples of Possible Silicone Sources | Possible Source |
|---|---|
| Silicone-based defoaming additives associated with cooking oil | Cooking areas using frying oil |
| Silicone in defoamers | Defoamers used in cooling-tower water treatment |
| Phenyl silicone | Heat-resistant lubricants or greases used around high-temperature drying or baking equipment |
| Heat-resistant silicone-containing waste oil | Waste-oil heaters |
| Silicone in mold release agents | Aluminum die-casting processes |
| Silicone in hair sprays or styling products | Break rooms or changing areas |
When airborne contamination is suspected, investigate the relationship between possible contaminant sources and the location of air intakes supplying the paint booth.
Wet-on-wet coating systems are generally designed so that each successive coating can wet and spread properly over the previous layer. Surface-energy and formulation balance between primer, intermediate coat, and topcoat therefore matter.
These formulations differ among paint manufacturers, and even coatings used for the same layer can have different surface characteristics.
If coatings from different manufacturers are sprayed simultaneously in the same booth, airflow disturbances caused by booth conditions or maintenance issues can carry overspray from one coating onto another painted surface. If the overspray has surface properties incompatible with the wet coating film, cratering may occur.
Partially dried mist deposited on booth walls, robots, hoses, or other equipment can create a similar problem if it later transfers to the painted surface.
In such cases, the investigation should include booth airflow, booth maintenance, overspray control, and whether simultaneous coating operations should be separated.
When one coating in a primer, intermediate-coat, and topcoat system is replaced with a product from another manufacturer, the wetting balance between layers may change. If the next coating does not wet the underlying layer properly, cratering can occur. Compatibility should therefore be evaluated for the complete coating system rather than for each paint in isolation.
When tools such as paint-can openers are reused without removing adhering paint, a low-surface-tension coating can be carried into another paint container and cause contamination. The same issue can occur with poorly cleaned funnels and other shared tools.
Waterborne emulsion coatings can contain coalescing agents. These components may volatilize in a preheating zone, condense on cooler parts of heat exchangers in a cooling zone, and form droplets. If the droplets are carried by airflow and deposit on the workpiece, they may interfere with wetting of a subsequently applied coating and cause cratering.
Silicone- and fluorine-based coatings generally have low surface energy, and residues or uncured overspray from these materials can interfere with the wetting of conventional coatings. Where cross-contamination cannot be adequately controlled, dedicated equipment or dedicated lines may be preferable.
When a defoamer is required, excessive addition can itself become a contamination source. Add only the amount needed for the process and manage concentration in accordance with the chemical supplier's instructions.
Cratering has occurred when painted parts were transported in reusable containers padded with printed advertising inserts or other materials, and contaminants transferred from the padding to the areas that later exhibited defects.
Stainless-steel mesh can carry processing oils or lubricants from manufacturing. Before using a new mesh for paint filtration, confirm its cleanliness and, where necessary, clean it using a method compatible with the mesh and coating process.
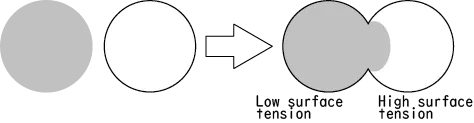
When investigating cratering, it is useful to determine whether a suspected material has lower surface tension than the paint and whether it causes the coating to recede. The following examples illustrate screening approaches for liquid samples and fine airborne contaminants.
| Place small droplets of the two liquids on a clean stainless-steel plate so that the droplets contact each other. Use clean sampling tools that will not introduce contamination. Observe how the liquids interact. A liquid with lower surface tension may spread differently against a higher-surface-tension liquid, providing a comparative indication of which sample is more likely to disturb paint wetting. This is a screening method rather than a quantitative surface-tension measurement. |
 |
| A practical screening approach is to prepare a clean test panel with a wet coating film and expose it briefly in a suspected area while observing the surface. A dark or metallic coating can make small surface defects easier to identify. |
| If crater-like depressions appear in the wet film, airborne contamination may be present in that environment. |
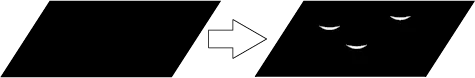 |
| The test panel can be used at suspected locations to compare where defects occur and to check whether corrective actions have reduced the problem. Results should be interpreted together with process conditions, airflow, materials, and contamination-control information. |
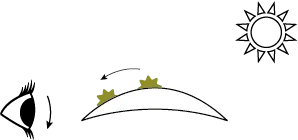
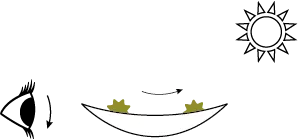
| When a defect is very small, it can be difficult to determine whether it is a depression caused by cratering or a raised particle defect. | |
| Reflected linear lighting can help distinguish concave and convex defects because the reflected image moves differently as the viewing angle changes. This simple optical check can be used as a preliminary screening technique before more detailed inspection. | |
|
|
 |
Product Information
|
|---|---|
 |
Technical Solutions
|
| Please be as specific as possible in your inquiry. Depending on the contents of your inquiry, it may take some time for us to reply to you. If you need product documentation (SDS/safety data sheets, TDS, instruction manuals, etc.), please contact us via “Request for SDS and other product documentation” ※Sales message through the inquiry form are strictly prohibited. |
KAKEN TECH, MICROCLEANER, MICROCLEAN&MARKLESS and MARKLESS are trademarks of KAKEN TECH CO., LTD. in PRC.
KAKEN TECH is a trademark of KAKEN TECH CO., LTD. in the U.S..
 Inquiry form
