- Company
- Products
- Technical report
- Indusrial cleaning
- Micro Joining and Assembly Technology
- Ultrasonic technology
- Trouble solution
- Cleaning
- Removing
- Attaching
- PCB Columns
Published on :
Conductive adhesives and silver pastes are attracting increasing attention, but incorrect handling can prevent them from delivering their intended performance.
This page explains how to use conductive adhesives, using thermosetting and solvent-drying types as examples. It covers the basic steps of thawing, cleaning, dispensing, and curing or drying, together with important handling points.
A conductive adhesive is an adhesive that conducts electricity. Many products contain silver as the conductive filler and are therefore also called silver paste or silver-filled conductive adhesive.
Because conductive adhesives can bond certain metals, resins, and other materials that may be difficult to solder, they are used in a wide range of applications.
As the use of heat-sensitive films and resins has increased, conductive adhesives have expanded as an alternative conductive joining method where soldering temperatures may be unsuitable.
This page uses KAKEN TECH's TK PASTE Series as an example to explain the basic handling procedure.
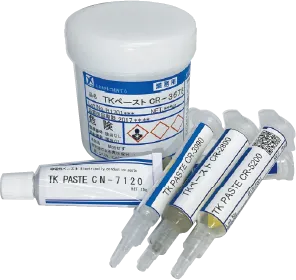
Thermosetting conductive adhesives bond through a heat-induced curing reaction of the resin. They are also referred to as heat-curing conductive adhesives and generally provide strong adhesion and good electrical conductivity.
Epoxy-based formulations are particularly common because of their heat resistance and bonding properties.
When the workpiece can tolerate heating around 100℃, an epoxy-based thermosetting type may be a suitable option, subject to the requirements of the actual application.
| Product | CR-2800 | CR-5200 | CR-3520 |
|---|---|---|---|
| Features | Low-Temperature Curing | Low-Temperature Curing Low-Resistance Bonding |
Good Heat Resistance |
| Typical Applications | Grounding Shielding |
Electronic Component Bonding |
Die Bonding |
| Resin | Epoxy | Epoxy | Epoxy |
| Volume Resistivity | 6×10⁻³ Ω・cm | 2×10⁻⁴ Ω・cm | 4×10⁻⁵ Ω・cm |
| Thermal Conductivity | ー | ー | 20 W/m・K |
| Curing Conditions | 90℃ ×60 min | 100℃ ×60 min | 130℃ ×30 min + 180℃ ×60 min |
| Storage | Frozen (below -10℃) | ||
| Package | 10g 5cc Syringe |
10g 5cc Syringe |
5g 3cc Syringe |
 |
[Thawing] Thaw the frozen conductive adhesive while keeping the container tightly sealed. Leave it at room temperature for at least 30 minutes. Before opening, wipe away any condensation from the outside of the container. Thaw at room temperature. Do not force-thaw the product using hot water, a hot plate, oven, hair dryer, or other direct heating method. Prevent condensation from entering the adhesive. Opening the cap while the container is still cold can allow moisture to enter and may adversely affect the material. |
|---|---|
 |
[Cleaning] Clean the bonding area with a suitable solvent such as alcohol or acetone, where compatible with the substrate. Flux residue, oil, and other contamination can reduce electrical and bonding performance. Allow the cleaning solvent to dry completely before applying the adhesive. |
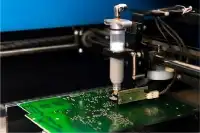 |
[Dispensing] Apply an appropriate amount of adhesive. A dispenser can help control deposit volume and placement accurately. Select a needle with an internal diameter appropriate for the adhesive. A needle that is too small may clog. After dispensing, proceed to curing promptly. Excessive delay before curing can affect final performance. Temperature and humidity in the work environment can affect handling and performance. For the products described here, a working temperature of 25℃ or below is recommended. |
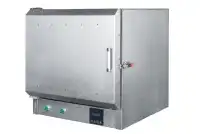 |
[Curing] Thermosetting conductive adhesives develop their intended properties through heat curing. Use a temperature-controlled oven and cure according to the recommended conditions for each product. Use an oven capable of maintaining a stable and uniform temperature. Hot plates and hair dryers may heat the workpiece unevenly. Curing behavior varies with temperature, time, applied amount, workpiece thermal mass, and oven loading. Validate the curing profile using the actual equipment, substrate, bond geometry, and production conditions. |
Solvent-drying conductive pastes become conductive as the solvent evaporates and the applied material dries and solidifies.
Compared with thermosetting conductive adhesives, their bonding strength may be lower, so they are often used together with another mechanical joining method such as screw fastening.
Because they can dry at room temperature, they can be suitable for particularly heat-sensitive materials.
| Product | CN-7120 | CN-7122S | ||
|---|---|---|---|---|
| Features | Room-Temperature Drying | Slower Drying | ||
| Typical Applications | Grounding Shielding |
|||
| Resin | Thermoplastic Resin | |||
| Volume Resistivity | 5×10⁻⁴ Ω$00B7cm | |||
| Thermal Conductivity | $2014 | |||
| Drying Conditions | Temperature | Guide Time | Temperature | Guide Time |
| 25℃ | 60 min | 25℃ | 120 min | |
| 40℃ | 10 min | 40℃ | 20 min | |
| 60℃ | 5 min | 60℃ | 10 min | |
| Storage | Frozen (below -10℃) | |||
| Package | 16g Aluminum Tube | |||
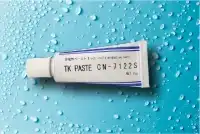 |
[Thawing] Thaw the frozen conductive paste while keeping the container tightly sealed. Leave it at room temperature for at least 30 minutes and wipe away external condensation before opening. Do not force-thaw the product using direct heating, and prevent condensation from entering the paste. |
|---|---|
|
[Cleaning] Clean the application area with a suitable solvent such as alcohol or acetone, where compatible with the substrate. Allow the cleaning solvent to dry completely before applying the paste. |
|
[Dispensing] Apply an appropriate amount of paste. Select a needle with an internal diameter appropriate for the paste. For the products described here, a working temperature of 25℃ or below is recommended. |
|
[Drying] Solvent-drying conductive pastes develop their intended properties as the solvent evaporates. Dry according to the recommended conditions. Drying behavior varies with temperature, time, applied amount, ventilation, workpiece geometry, and oven loading. Validate the drying conditions using the actual equipment and materials. |
Even when the same conductive adhesive is used, electrical conductivity and adhesion can vary depending on storage conditions, thawing method, the surface condition of the adherend, the applied amount, and curing or drying conditions. To achieve stable performance, it is important to control not only the adhesive itself but also the entire handling and application process.
Conductive adhesives should be stored at the temperature specified for each product to minimize reactions during storage, solvent loss, and changes in material condition. Some TK PASTE products require frozen storage. Check the storage requirements before use and maintain the specified temperature.
Conductive adhesives stored frozen should be thawed at room temperature while the container remains tightly sealed. Opening a cold container may allow moisture from the air to condense and enter the adhesive. Allow the container to warm sufficiently, wipe off any condensation from the outside, and then open it.
Avoid forced thawing using hot water, a hot plate, oven, hair dryer, or other direct heating method.
Oil, flux residue, and other contamination remaining on the adherend can affect electrical conductivity and bond strength. Before applying the adhesive, clean the bonding surface using a cleaning agent compatible with the adherend and allow it to dry completely.
Performance after bonding can vary with the applied amount and bond-line condition. In mass production, a dispenser can help keep the dispensing position and amount consistent. Select a needle diameter appropriate for the adhesive viscosity and conductive particle size.
For thermosetting types, consider not only the oven set temperature but also whether the adhesive itself reaches the required temperature. Heating behavior varies with the applied amount, the material and size of the adherend, and oven loading.
For solvent-drying types, solvent evaporation also varies with temperature, time, and applied amount. Use the published conditions as a reference, then evaluate the adhesive with the actual equipment, materials, and application amount.
Conductive adhesive performance is affected by adherend material, surface condition, application method, bonding area, and curing conditions. Before mass production, evaluate electrical conductivity, bond strength, curing or drying condition, and other required properties using the actual materials and equipment.
 |
Product Information
|
|---|
 |
Technical Solutions
|
|---|---|
|
Technical Solutions
|
 |
Product Information
|
 |
Product Information
|
| Please be as specific as possible in your inquiry. Depending on the contents of your inquiry, it may take some time for us to reply to you. If you need product documentation (SDS/safety data sheets, TDS, instruction manuals, etc.), please contact us via “Request for SDS and other product documentation” ※Sales message through the inquiry form are strictly prohibited. |
KAKEN TECH, MICROCLEANER, MICROCLEAN&MARKLESS and MARKLESS are trademarks of KAKEN TECH CO., LTD. in PRC.
KAKEN TECH is a trademark of KAKEN TECH CO., LTD. in the U.S..
 Inquiry form
