- Company
- Products
- Technical report
- Film-Type Perovskite Solar Cells
- Indusrial cleaning
- Micro Joining and Assembly Technology
- Ultrasonic technology
- Trouble solution
- Cleaning
- Removing
- Attaching
- PCB Columns
Published on :
A conductive adhesive is, as the name suggests, an adhesive that conducts electricity. Conductive adhesives containing silver fillers are also commonly referred to as silver paste.
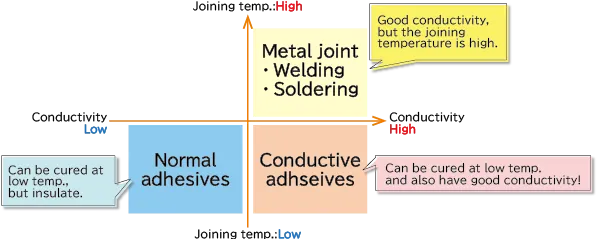
How do they differ from conventional adhesives and solder used to join electronic components? One useful way to compare them is by looking at joining temperature and electrical conductivity.
Metal joining methods such as welding and soldering provide excellent electrical conductivity but generally require relatively high joining temperatures. Conventional adhesives can often be bonded at lower temperatures, but most are electrically insulating.
Conductive adhesives provide both bonding and electrical conductivity and can often be processed at lower temperatures than solder. For this reason, they are attracting attention as an alternative joining technology in applications where soldering is difficult.
 |
Solder has traditionally been widely used for electrically conductive joining of electronic components. However, as electronic devices become smaller, lighter, and more diverse, including wearable devices, an increasing number of components and circuits use heat-sensitive resins and film materials instead of conventional metal, glass, or ceramic substrates. As a result, demand is increasing for electrically conductive joining materials that can be processed at lower temperatures. Conductive adhesives can provide conductive bonding at lower temperatures than many soldering processes, making them useful for joining heat-sensitive resin and film components. |
Conductive adhesives (silver pastes) and solder are both used for electrically conductive joining, but their processes and material properties differ. The following sections summarize representative advantages and limitations of conductive adhesives.
| Can be joined at lower temperatures than solder in many applications |
| Soldering processes can require relatively high temperatures, while some conductive adhesives are designed to cure below 100℃. Lower-temperature processing can enable conductive joining of heat-sensitive materials such as resins and films. Lower processing temperatures may also reduce process energy consumption depending on the curing conditions and production system. |
| Can bond materials that are difficult to solder |
| Materials such as stainless steel and aluminum can be difficult to solder because of stable surface oxide films. Conductive adhesives rely on adhesion by the binder resin rather than formation of a solder alloy. However, surface condition still affects adhesive bonding, so surface preparation and compatibility should be evaluated for the actual substrate. |
| No solder remelting |
| A solder joint can remelt if it is subsequently heated above the solder alloy's melting range. This can lead to component movement during later thermal processes. Thermosetting conductive adhesives form a cured polymer network rather than a solder alloy, so they do not undergo solder-like remelting after proper curing. |
| No soldering flux residue |
| Soldering flux is used to remove or control oxide films and support solder wetting. After soldering, flux residue may remain and may require cleaning depending on the flux, product design, downstream processes, and reliability requirements. Conductive adhesives do not require soldering flux for the bonding mechanism, so soldering-flux residue is not generated by the conductive adhesive joining process itself. |
| Large reflow ovens may not be required |
| Mass-production SMT soldering commonly uses reflow ovens, which can require substantial installation space. Conductive adhesives are cured or dried using equipment selected according to the adhesive chemistry, curing profile, workpiece size, and throughput, and some applications can use more compact thermal equipment. |
| Curing can take longer than soldering |
| Soldering can complete the joining process relatively quickly, while thermosetting conductive adhesives may require longer heating or curing times. Actual curing time varies significantly with formulation, temperature, bond-line geometry, and required properties, so the manufacturer's recommended curing profile should be followed. |
| Material cost can be higher |
| Many conductive adhesives use silver as the electrically conductive filler. Because silver is a high-value material, the material cost can be higher than that of some solder alloys. Actual cost depends on silver content, formulation, packaging, application amount, and production conditions. |
| No solder-like self-alignment effect |
| During solder reflow, surface tension of molten solder can help pull components toward the intended pad position. This is known as the self-alignment effect. Conductive adhesives generally do not provide the same molten-solder self-alignment mechanism, so placement accuracy and fixation during curing become more important. |
| Mechanical strength differs from solder joints |
| Solder creates a metallurgical joint, whereas conductive adhesives bond through a polymer matrix containing conductive filler. Mechanical properties therefore differ from solder and depend strongly on the adhesive formulation, substrate, surface treatment, bond geometry, and curing conditions. Suitability should be confirmed against the required mechanical reliability of the application. |
| The main component of a conventional adhesive is typically an electrically insulating polymer resin. Conductive adhesives disperse conductive particles, also called conductive fillers, in an organic binder such as epoxy resin. As the binder cures and the conductive particles come into sufficiently close contact, electrically conductive pathways are formed through the adhesive. |
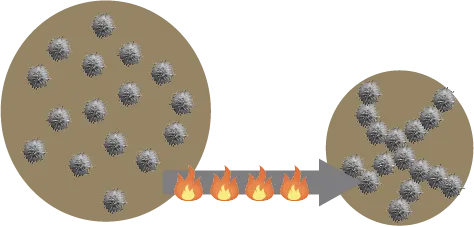
As the binder resin cures, conductive particles form contacting pathways that allow electrical current to flow. |
| This conduction mechanism differs from solder, where a metallic solder alloy melts and forms a metallurgical joint. The conductive particles in a conductive adhesive generally do not melt together. A sufficient amount of conductive filler is therefore required for particles to form a continuous conductive network. The conceptual diagram below illustrates the relationship between conductive filler content and electrical conductivity. At low filler loading the particles remain electrically isolated, while conductivity rises sharply once a connected network begins to form. Beyond a certain filler level, further increases may produce progressively smaller improvements in conductivity. |
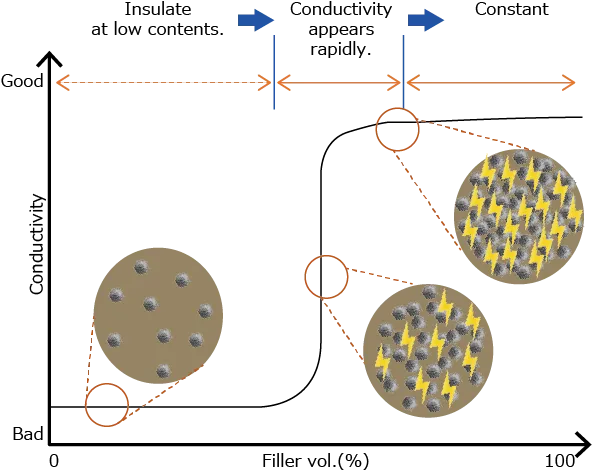
Conductivity emerges as conductive particles form a connected network within the resin matrix. [1] |
| Many types of organic binder resins and conductive fillers are available, and manufacturers offer a wide range of conductive adhesive formulations. Selection should consider required electrical performance, adhesion, operating environment, application method, curing conditions, reliability, and cost. |
| For electronic component joining, heat-curing epoxy conductive adhesives containing silver filler are widely used. Epoxy resins can provide good adhesion to many materials, thermal resistance, and relatively low curing shrinkage. Silver is also widely used in electronic materials because of its high electrical and thermal conductivity and relatively stable conductive performance. |
| Conductive adhesives commonly use spherical, flake-shaped, or other forms of silver conductive filler. Particle size, morphology, surface treatment, and filler loading are adjusted according to the required rheology, conductivity, adhesion, and process characteristics. For this reason, silver-filled conductive adhesives are often called “silver paste.” |
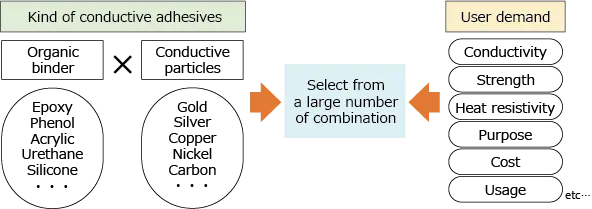
A wide variety of conductive adhesives can be formulated by combining different binder resins and conductive fillers. Selection should be based on performance, application, process, and cost requirements. |
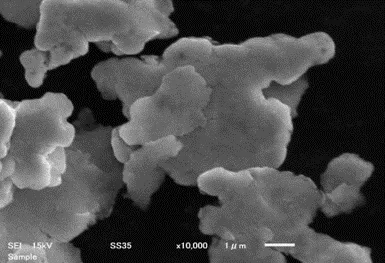 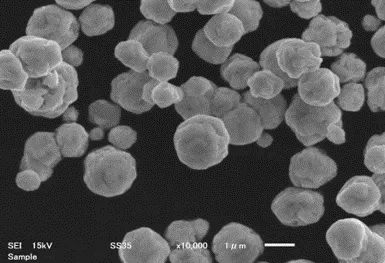
Conductive adhesives for electronic components commonly use silver fillers with shapes such as flakes and spheres. |
 |
Technical Solutions
|
|---|---|
 |
Technical Solutions
|
 |
Product Information
|
 |
Product Information
|
The information on this page reflects KAKEN TECH's technical perspective and is not intended to define or cover every conductive adhesive technology or product.
The original technical content of this article is based on information available as of December 2022.
| Please be as specific as possible in your inquiry. Depending on the contents of your inquiry, it may take some time for us to reply to you. If you need product documentation (SDS/safety data sheets, TDS, instruction manuals, etc.), please contact us via “Request for SDS and other product documentation” ※Sales message through the inquiry form are strictly prohibited. |
KAKEN TECH, MICROCLEANER, MICROCLEAN&MARKLESS and MARKLESS are trademarks of KAKEN TECH CO., LTD. in PRC.
KAKEN TECH is a trademark of KAKEN TECH CO., LTD. in the U.S..
 Inquiry form

